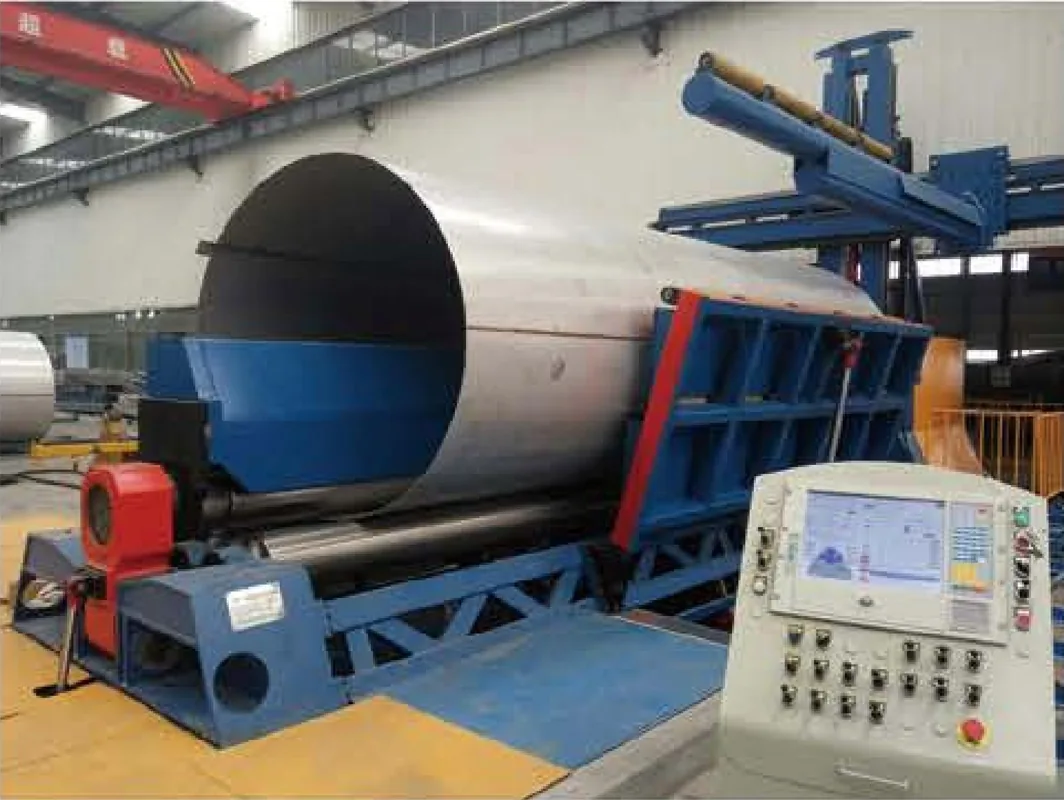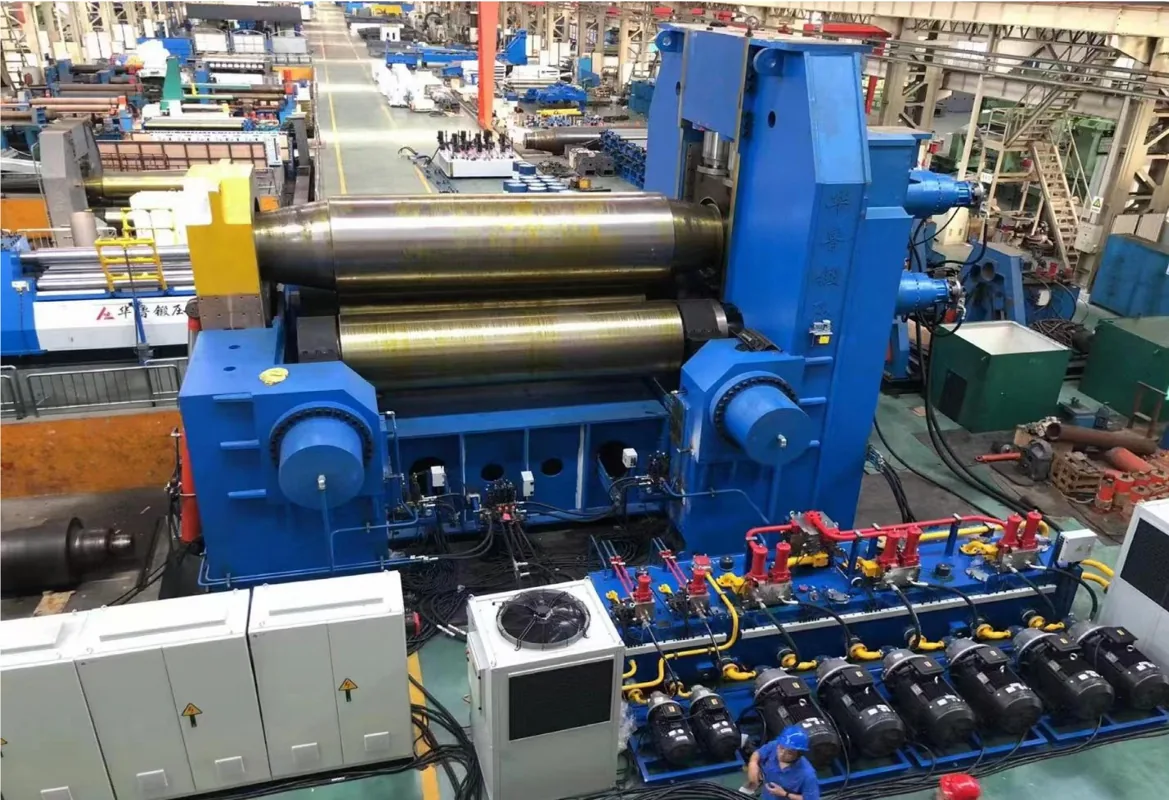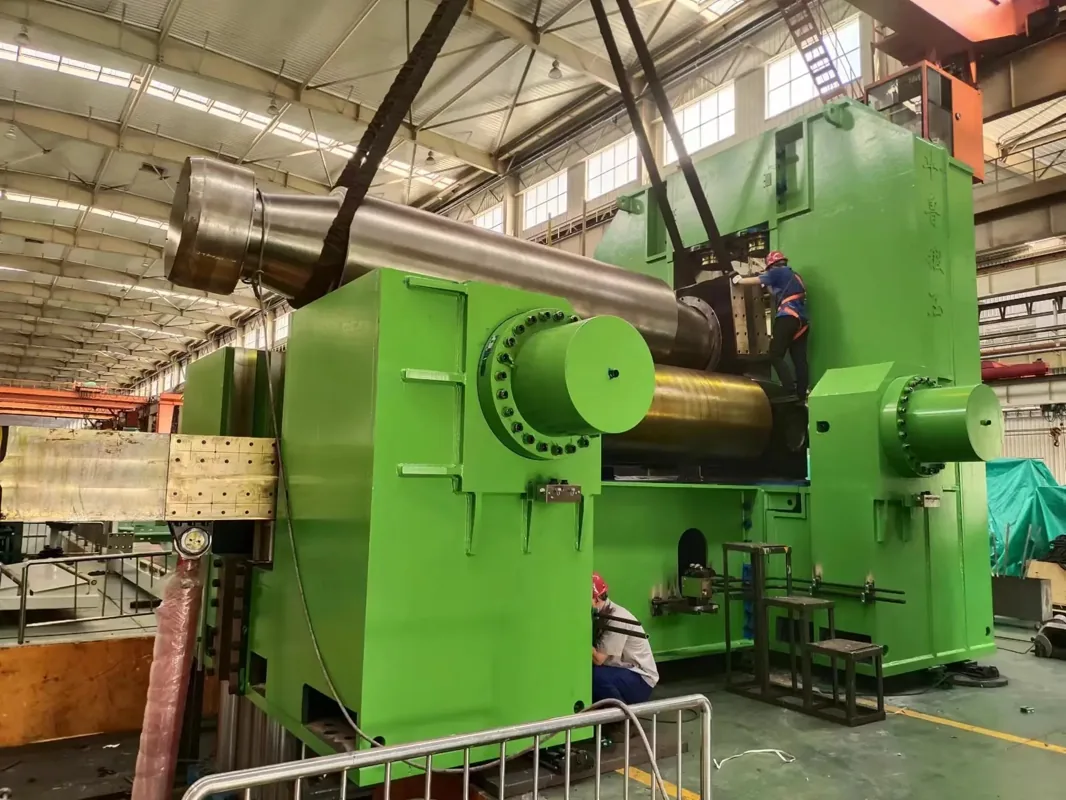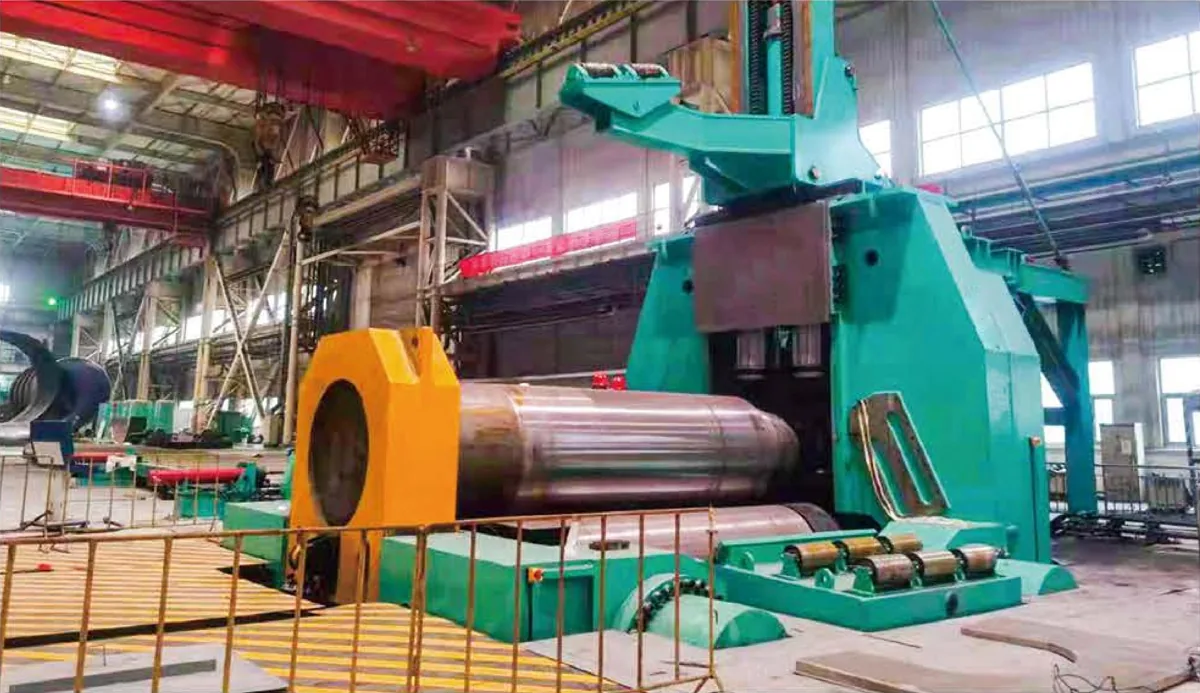
Product Overview
For Shipbuilding Plate Press Brake, the buying team usually wants the quotation tied to the drawing, the workshop layout and the inspection plan. Engineers should check tonnage, bending length, crowning, backgauge repeatability and tooling match; procurement managers should compare the complete quoted scope for Shipbuilding Plate Press Brake; production directors should confirm whether the equipment can keep stable output; workshop operators should review operator reach, tooling changeover, part support, safety light curtain and maintenance access before approval.
What the Buying Team Should Confirm
| Role | Decision Point | Why It Matters |
|---|---|---|
| Engineer | tonnage, bending length, crowning, backgauge repeatability and tooling match | Verifies the technical route for Shipbuilding Plate Press Brake before the supplier shortlist is narrowed. |
| Procurement Manager | The procurement manager should verify Shipbuilding Plate Press Brake scope, options, documents, spare parts and service responsibility before shortlist approval. | It helps buyers judge Shipbuilding Plate Press Brake by scope, options, documents and service responsibility. |
| Production Director | angle consistency, crowning result, backgauge accuracy and re-bend avoidance | Helps confirm that Shipbuilding Plate Press Brake can keep output stable across shifts after installation. |
| Workshop Operator | operator reach, tooling changeover, part support, safety light curtain and maintenance access | Makes day-to-day use of Shipbuilding Plate Press Brake easier for the shop floor team. |
Best-Fit Workshop Scenarios
Good Fit
Shipbuilding Plate Press Brake is worth reviewing when the buyer can define bending length, tonnage, plate thickness, V-opening, backgauge requirement and part geometry and needs a machine route tied to production evidence.
Risk to Clarify
For Shipbuilding Plate Press Brake, vague information about tonnage, bending length, crowning, backgauge repeatability and tooling match can make quoted models look similar on paper while behaving differently in production.
Evidence to Request
For Shipbuilding Plate Press Brake, ask Hualu Equipment to state capacity assumptions, support-device scope, control functions, trial-run items, packing method and documentation.
Configuration Choices That Affect Shipbuilding Plate Press Brake Price and Output
| Configuration Area | Buyer Question | Practical Impact |
|---|---|---|
| Machine Structure | Is the press brake equipment structure sized for bending length, tonnage, plate thickness, V-opening, backgauge requirement and part geometry? | For Shipbuilding Plate Press Brake, structure choice affects rigidity, repeatability and long-term stability. |
| Support and Handling | Which support, feeding, stacking, tooling or handling items are included for Shipbuilding Plate Press Brake? | This controls whether Shipbuilding Plate Press Brake can be loaded, watched and unloaded in the buyer's real workshop. |
| Control System | Which CNC, PLC, hydraulic, backgauge or automation functions are included for Shipbuilding Plate Press Brake? | For Shipbuilding Plate Press Brake, control scope affects repeatability, operator workload and shift-to-shift consistency. |
| Acceptance Scope | What will Hualu Equipment test for Shipbuilding Plate Press Brake before shipment, and what evidence can the buyer review? | For Shipbuilding Plate Press Brake, clear acceptance scope reduces ambiguity before payment, packing and installation. |
Selection Priorities for Shipbuilding Plate Press Brake
- Start the shipbuilding press brake route with bending length plus the latest drawing revision.
- For the shipbuilding press brake route, the next check is tonnage requirement before the shortlist is narrowed.
- The workshop review for the shipbuilding press brake route should connect backgauge repeatability to downstream process and crane access.
- The final RFQ step for the shipbuilding press brake route is to request test items, inspection records, packing method, manuals and shipping documentation.
For the shipbuilding press brake route, the acceptance discussion should return to angle consistency, crowning result, backgauge accuracy and re-bend avoidance before commercial terms are signed off.
In Wind Energy, Marine and Shipyard, Oil and Gas, Pressure Vessel, Power Generation, Steel Service Centers, project success for the shipbuilding press brake route depends on planning as much as nominal capacity. For the shipbuilding press brake route, tooling, handling, calibration, training, spare parts, documentation and factory acceptance testing should be discussed before purchase so overseas buyers can evaluate project risk clearly.
Before approving drawing confirmation for the shipbuilding press brake route and the press brake equipment route, the procurement manager needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team reduce rework before welding and inspection.
During spare parts review on the shipbuilding press brake route, the welding engineer should compare bending length with the drawing, material data and production target so the project team can give operators clearer acceptance criteria.
At hydraulic service planning against the current drawing package for the shipbuilding press brake route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to avoid a mismatch between drawings and acceptance criteria.
At final commercial comparison on the shipbuilding press brake route, the plant manager still needs to verify operator reach so the project team can compare suppliers on measurable evidence.
The workshop operator should record tooling compatibility during factory acceptance testing on the shipbuilding press brake route, because that single check can help the workshop protect production rhythm during peak workload on this project.
When production ramp-up is discussed against the current drawing package for the shipbuilding press brake route, crowning and angle control should be checked by the shipping coordinator against the real press brake equipment route, which helps the project team keep maintenance access practical after commissioning.
At remote support planning under the shop-floor constraint of the shipbuilding press brake route, the maintenance supervisor's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop prepare a more accurate RFQ package.
Before approving pre-contract clarification against the current drawing package for the shipbuilding press brake route, the after-sales coordinator needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team keep spare parts planning realistic.
Configuration Scope for Shipbuilding Plate Press Brake
Procurement teams should compare the complete scope behind the quotation. For the shipbuilding press brake route, the complete scope may need feeding support, side support, top support, tooling, CNC functions, safety guarding, spare parts, manuals and operator training so the shop receives a working cell rather than an isolated machine.
A useful RFQ for the shipbuilding press brake route should let an engineer reproduce the job conditions. For the shipbuilding press brake route, required data include bending length, tonnage, plate thickness, V-opening, backgauge requirement and part geometry, giving Hualu Equipment enough context to prepare a practical response.
At factory acceptance testing for the shipbuilding press brake route and the press brake equipment route, the production director's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop compare suppliers on measurable evidence.
Before approving production ramp-up under the shop-floor constraint of the shipbuilding press brake route, the plant manager needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team protect production rhythm during peak workload.
During remote support planning under the shop-floor constraint of the shipbuilding press brake route, the workshop operator should compare bending length with the drawing, material data and production target so the project team can keep maintenance access practical after commissioning.
At pre-contract clarification for the shipbuilding press brake route and the press brake equipment route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to prepare a more accurate RFQ package.
At shipment planning on the shipbuilding press brake route, the maintenance supervisor still needs to verify operator reach so the project team can keep spare parts planning realistic.
The after-sales coordinator should record tooling compatibility during quality inspection under the shop-floor constraint of the shipbuilding press brake route, because that single check can help the workshop confirm shipment limits before final packing on this project.
When capacity verification is discussed against the current drawing package for the shipbuilding press brake route, crowning and angle control should be checked by the quality inspector against the real press brake equipment route, which helps the project team shorten technical clarification before contract signing.
At site readiness review for the shipbuilding press brake route and the press brake equipment route, the engineer's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop identify missing workshop utilities earlier.
Workshop Use for Shipbuilding Plate Press Brake
When a quotation is prepared, Hualu Equipment links the proposal for the shipbuilding press brake route to factory capability, process assumptions, test items and documents that the buyer can request for review.
For the production director, the real question on the shipbuilding press brake route is whether the line will keep output stable across shifts. For the shipbuilding press brake route, the acceptance discussion should focus on tonnage, bending length, crowning, backgauge repeatability and tooling match, not on model naming alone.
When shipment planning is discussed under the shop-floor constraint of the shipbuilding press brake route, crowning and angle control should be checked by the workshop operator against the real press brake equipment route, which helps the project team prepare a more accurate RFQ package.
At quality inspection on the shipbuilding press brake route, the shipping coordinator's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop keep spare parts planning realistic.
Before approving capacity verification on the shipbuilding press brake route, the maintenance supervisor needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team confirm shipment limits before final packing.
During site readiness review against the current drawing package for the shipbuilding press brake route, the after-sales coordinator should compare bending length with the drawing, material data and production target so the project team can shorten technical clarification before contract signing.
At installation preparation against the current drawing package for the shipbuilding press brake route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to identify missing workshop utilities earlier.
At welding preparation under the shop-floor constraint of the shipbuilding press brake route, the engineer still needs to verify operator reach so the project team can reduce avoidable questions during installation.
The project manager should record tooling compatibility during tooling review against the current drawing package for the shipbuilding press brake route, because that single check can help the workshop make the factory test easier to verify on this project.
When trial run planning is discussed against the current drawing package for the shipbuilding press brake route, crowning and angle control should be checked by the procurement manager against the real press brake equipment route, which helps the project team match the machine layout to the crane route.
Installation Notes for Shipbuilding Plate Press Brake
For shops in Wind Tower Manufacturing, Shipbuilding, Pressure Vessel Fabrication, Steel Structure Fabrication, Aerospace Plate Forming, Nuclear Power Equipment, the job usually centers on keeping rework down before welding, inspection and final assembly. For the shipbuilding press brake route, high strength steel, marine grade steel, stainless steel, aluminum alloy, carbon steel, structural steel or explosion bonded plate each creates a different forming or processing margin.
For the workshop operator, equipment on the shipbuilding press brake route should be easy to load, watch, clean and maintain. On a busy press brake equipment line for the shipbuilding press brake route, access around the machine, clear control logic and predictable motion matter as much as nominal capacity.
The maintenance supervisor should record tooling compatibility during installation preparation for the shipbuilding press brake route and the press brake equipment route, because that single check can help the workshop shorten technical clarification before contract signing on this project.
When welding preparation is discussed under the shop-floor constraint of the shipbuilding press brake route, crowning and angle control should be checked by the after-sales coordinator against the real press brake equipment route, which helps the project team identify missing workshop utilities earlier.
At tooling review on the shipbuilding press brake route, the quality inspector's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop reduce avoidable questions during installation.
Before approving trial run planning under the shop-floor constraint of the shipbuilding press brake route, the engineer needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team make the factory test easier to verify.
During operator training under the shop-floor constraint of the shipbuilding press brake route, the project manager should compare bending length with the drawing, material data and production target so the project team can match the machine layout to the crane route.
At foundation approval for the shipbuilding press brake route and the press brake equipment route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to avoid buying capacity that cannot be used in the workshop.
At crane access review on the shipbuilding press brake route, the welding engineer still needs to verify operator reach so the project team can reduce installation delays after delivery.
The production director should record tooling compatibility during quotation review for the shipbuilding press brake route and the press brake equipment route, because that single check can help the workshop separate essential options from optional accessories on this project.
RFQ Data for Shipbuilding Plate Press Brake
Heavy press brake equipment for the shipbuilding press brake route should be compared by structure, hydraulic response, machined working parts, control repeatability and operator access. For the shipbuilding press brake route, a proposal is stronger when it explains the drawing assumptions, material strength, capacity basis, support devices and acceptance method.
After installation, the most useful check for the shipbuilding press brake route is whether the machine matches angle consistency, crowning result, backgauge accuracy and re-bend avoidance. For the shipbuilding press brake route, drawings, trial pieces and final handover documents should agree before the buyer signs off.
At operator training for the shipbuilding press brake route and the press brake equipment route, the quality inspector still needs to verify operator reach so the project team can make the factory test easier to verify.
The engineer should record tooling compatibility during foundation approval under the shop-floor constraint of the shipbuilding press brake route, because that single check can help the workshop match the machine layout to the crane route on this project.
When crane access review is discussed for the shipbuilding press brake route and the press brake equipment route, crowning and angle control should be checked by the project manager against the real press brake equipment route, which helps the project team avoid buying capacity that cannot be used in the workshop.
At quotation review for the shipbuilding press brake route and the press brake equipment route, the procurement manager's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop reduce installation delays after delivery.
Before approving maintenance planning against the current drawing package for the shipbuilding press brake route, the welding engineer needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team separate essential options from optional accessories.
During electrical review for the shipbuilding press brake route and the press brake equipment route, the production director should compare bending length with the drawing, material data and production target so the project team can reduce rework before welding and inspection.
At documentation handover against the current drawing package for the shipbuilding press brake route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to give operators clearer acceptance criteria.
At drawing confirmation for the shipbuilding press brake route and the press brake equipment route, the workshop operator still needs to verify operator reach so the project team can avoid a mismatch between drawings and acceptance criteria.
Acceptance Checks for Shipbuilding Plate Press Brake
Maintenance and production staff should check lubrication access, cabinet layout, hydraulic service points, foundation loads, crane clearance and guarding before approval of the shipbuilding press brake route. For the shipbuilding press brake route, these details decide whether the machine can run smoothly after installation, especially when operators work across multiple shifts.
During quotation review against the current drawing package for the shipbuilding press brake route, the engineer should compare bending length with the drawing, material data and production target so the project team can avoid buying capacity that cannot be used in the workshop.
At maintenance planning on the shipbuilding press brake route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to reduce installation delays after delivery.
At electrical review on the shipbuilding press brake route, the procurement manager still needs to verify operator reach so the project team can separate essential options from optional accessories.
The welding engineer should record tooling compatibility during documentation handover for the shipbuilding press brake route and the press brake equipment route, because that single check can help the workshop reduce rework before welding and inspection on this project.
When drawing confirmation is discussed for the shipbuilding press brake route and the press brake equipment route, crowning and angle control should be checked by the production director against the real press brake equipment route, which helps the project team give operators clearer acceptance criteria.
At spare parts review for the shipbuilding press brake route and the press brake equipment route, the plant manager's review of backgauge repeatability is not paperwork. It shows whether the shipbuilding press brake route will help the workshop avoid a mismatch between drawings and acceptance criteria.
Before approving hydraulic service planning under the shop-floor constraint of the shipbuilding press brake route, the workshop operator needs to verify tonnage requirement; this keeps the purchase decision tied to shop-floor evidence and helps the team compare suppliers on measurable evidence.
During final commercial comparison for the shipbuilding press brake route and the press brake equipment route, the shipping coordinator should compare bending length with the drawing, material data and production target so the project team can protect production rhythm during peak workload.
At factory acceptance testing on the shipbuilding press brake route, the buyer should not stop at the checklist; the final handoff evidence must line up well enough to keep maintenance access practical after commissioning.
Shipbuilding Plate Press Brake RFQ Data
For a reliable technical response, send bending length, tonnage, plate thickness, V-opening, backgauge requirement and part geometry together with drawings, inspection requirements, destination country and any site constraints such as voltage, foundation, crane capacity or available floor space.
Customer Benefits
Engineering Fit
Shipbuilding Plate Press Brake is configured around the buyer's material, thickness, width, target geometry, tolerance and production requirement.
Factory Review
For Shipbuilding Plate Press Brake, buyers can request factory background, manufacturing photos, testing discussion and documentation through the related About pages.
Export Support
Shipbuilding Plate Press Brake inquiries can include technical communication, documents, video support, packing discussion and overseas project coordination.
Buyer Search Questions This Page Answers
Search data for Shipbuilding Plate Press Brake shows buyers using practical machine and application wording. This section keeps those queries tied to engineering decisions so the page can rank without turning Shipbuilding Plate Press Brake into a keyword-stuffed synonym page.
| Search Wording | What It Means for the RFQ |
|---|---|
| plate bending machine for shipbuilding | buyers need hull shell fit-up, marine plate support and crane handling for Shipbuilding Plate Press Brake |
| ship plate bending machine | buyers want pre-bending, shell transfer and weld prep clarified for Shipbuilding Plate Press Brake |
| shipbuilding plate forming equipment | buyers expect a whole route, not one machine name for Shipbuilding Plate Press Brake |
| marine steel plate forming machine | buyers want marine steel behavior, support devices and acceptance notes for Shipbuilding Plate Press Brake |
Decision Checks Behind These Searches
Engineering Review
Use drawings, material grade, yield strength, thickness, width and target geometry as the starting point for Shipbuilding Plate Press Brake.
RFQ Scope
Compare main machine, supports, CNC or hydraulic functions, documents, trial items, training and packing for Shipbuilding Plate Press Brake.
Supplier Shortlist
Judge the route by acceptance logic and shop-floor flow, not only by the machine name for Shipbuilding Plate Press Brake.
Engineering Considerations
For Shipbuilding Plate Press Brake, the engineering check should connect plate data, support devices, control method and FAT scope before the quote is compared.
Manufacturing and QC
For Shipbuilding Plate Press Brake, QC evidence should be tied to the real machine route the buyer will accept. For the shipbuilding press brake route, buyers can request machining checks, assembly photos, hydraulic testing, electrical cabinet review, trial running, support-device checks and a FAT list tied to the quoted configuration.
Applications and Industries
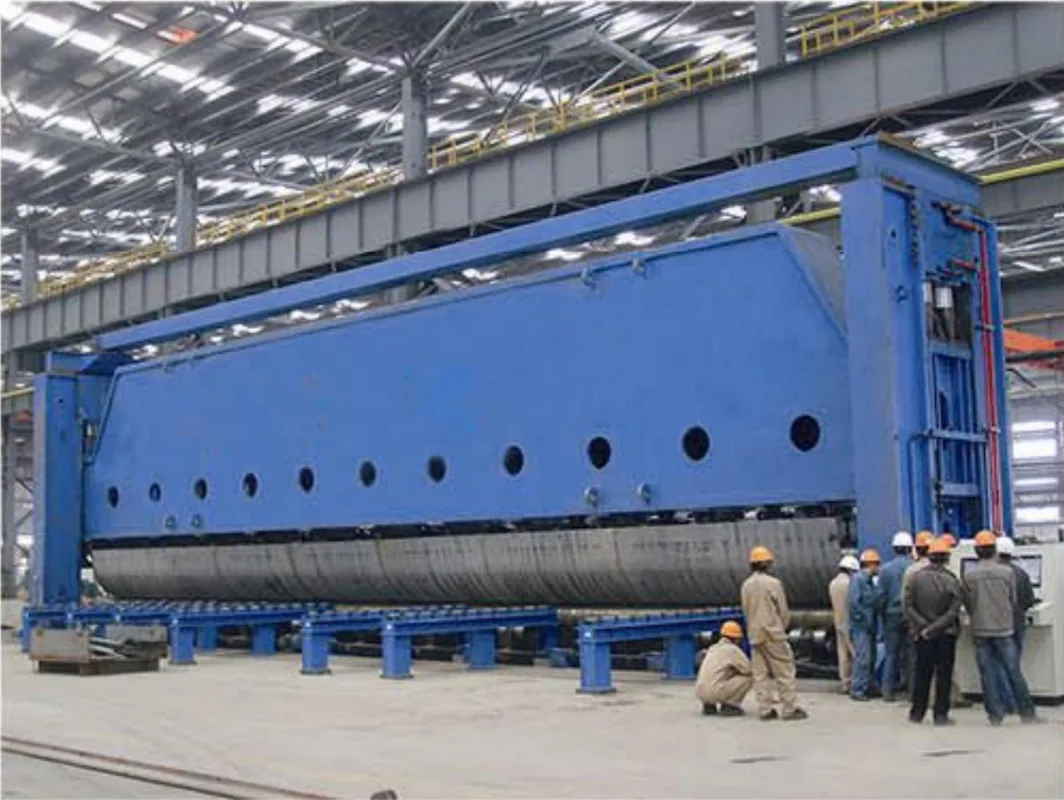
Shipbuilding
For the shipbuilding press brake route, buyers usually review shipbuilding, and buyers should check shell fit-up, pre-bending route, plate transport and welding handoff before requesting a proposal.
Offshore Engineering
For the shipbuilding press brake route, buyers usually review offshore engineering, and buyers should check corrosion-grade plate handling, safety access, crane route and delivery condition before RFQ.
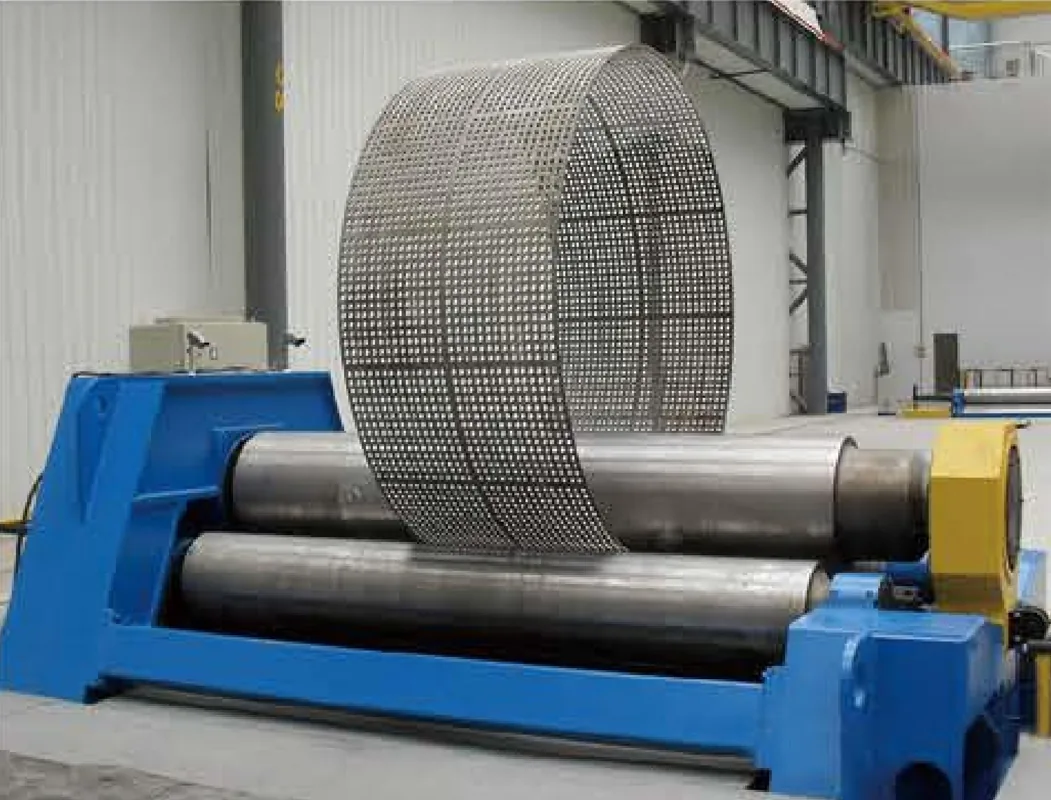
Pressure Vessel Fabrication
For the shipbuilding press brake route, buyers usually review pressure vessel fabrication, and buyers should check seam closure, roundness, nozzle fit-up and fit-up tolerance before comparing suppliers.
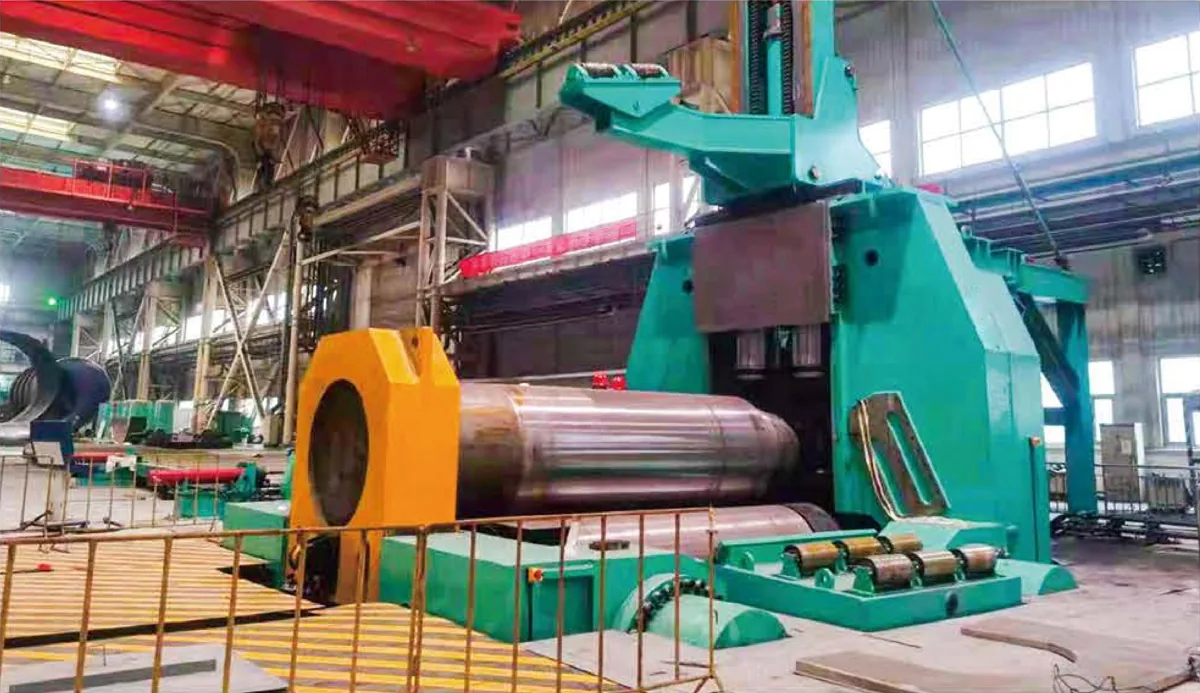
Wind Tower Manufacturing
For the shipbuilding press brake route, buyers usually review wind tower manufacturing, and buyers should check shell diameter, section transfer, top support layout and turn-around rhythm before approving the line.
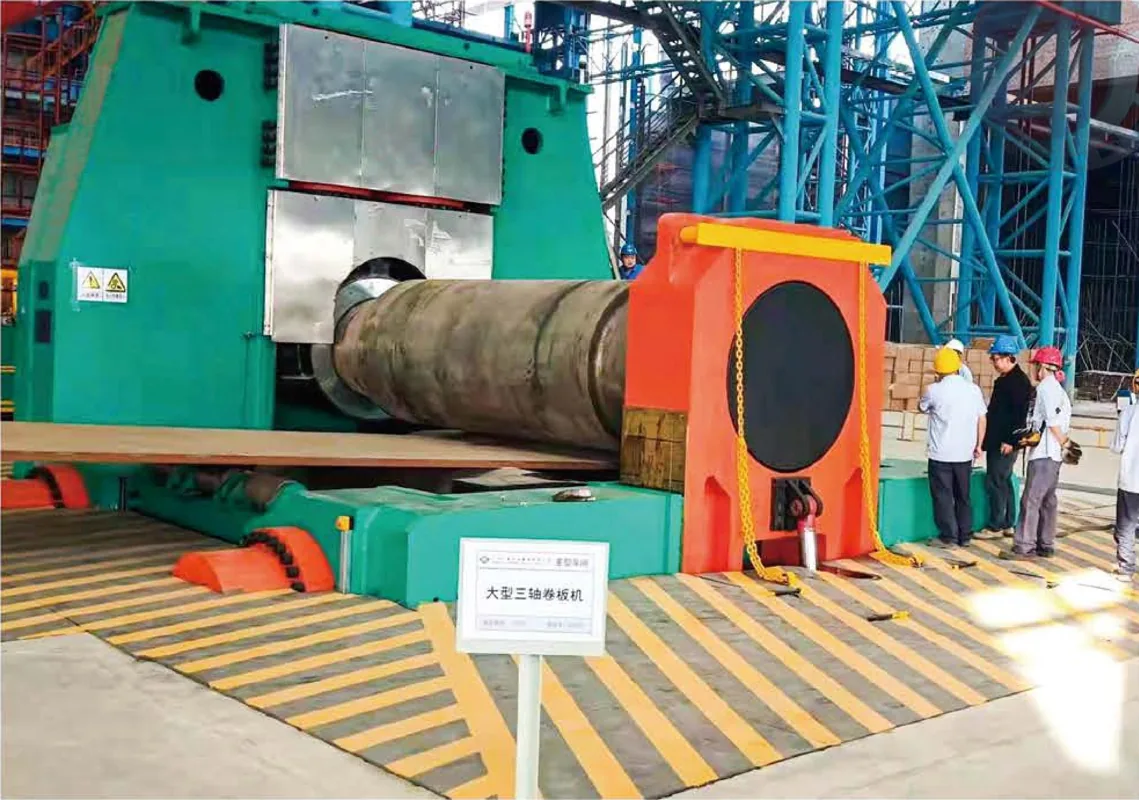
Heavy Fabrication
For the shipbuilding press brake route, buyers usually review heavy fabrication, and buyers should check material mix, handling route, output rhythm and operator access before comparison.
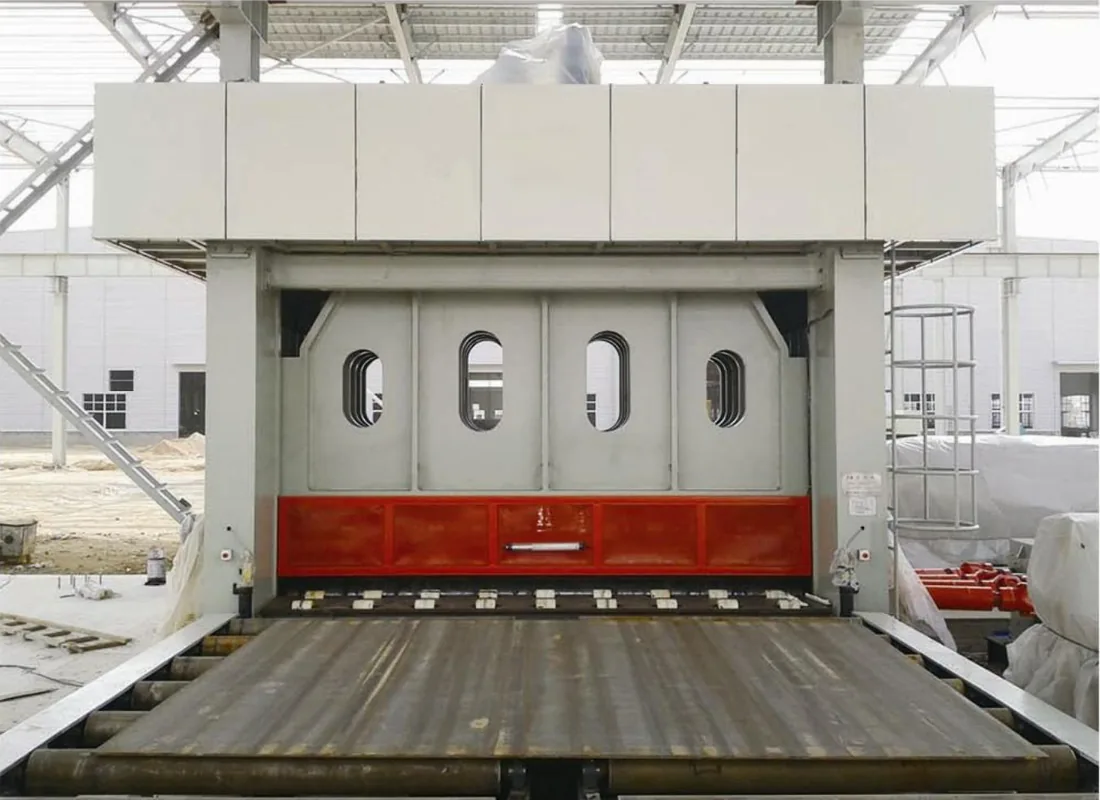
Steel Structure Fabrication
For the shipbuilding press brake route, buyers usually review steel structure fabrication, and buyers should check flatness, edge preparation, part flow and downstream assembly access before shortlisting equipment.
Technical Data to Prepare
| RFQ Item | Recommended Detail |
|---|---|
| Material | the shipbuilding press brake route - Grade, yield strength, thickness range and surface condition. |
| Plate Size | the shipbuilding press brake route - Width, length, minimum diameter, shell length or flatness target. |
| Production | the shipbuilding press brake route - Monthly output, shift pattern, automation need and downstream route. |
| Workshop | the shipbuilding press brake route - Power supply, crane capacity, foundation, space and packing limit. |